
ISO 5817 quality levels B, C and D: selecting and applying
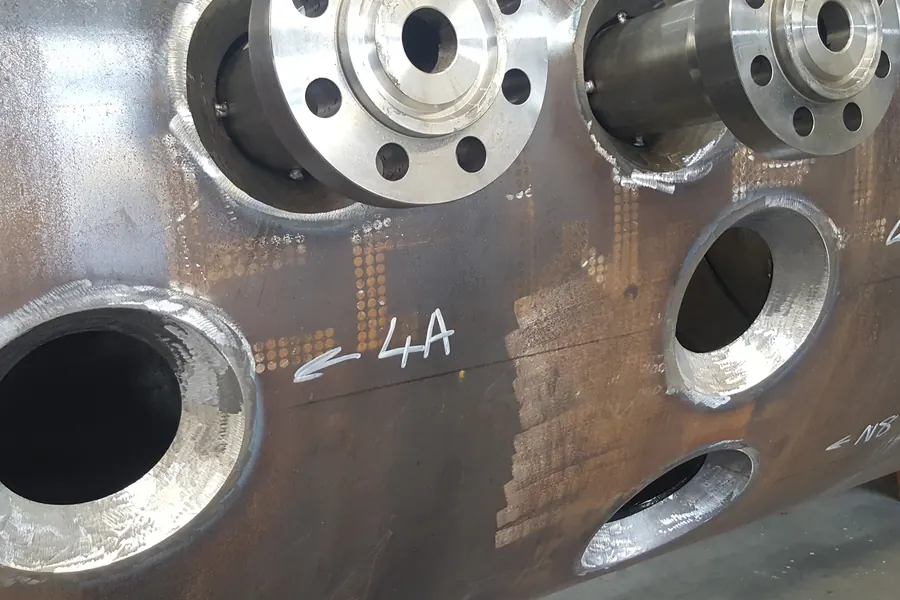
ISO 5817 is the standard used to assess weld imperfections in steel, nickel and titanium. It defines three quality levels: B (stringent), C (intermediate) and D (moderate). For each type of imperfection, from porosity and undercut to excess penetration and misalignment, the standard gives limit values per level. The level therefore determines which deviations are acceptable and which must be repaired.
The quality level is not a free choice for the workshop: it follows from the applicable standard or the contract, and it directly affects repair cost, lead time and inspection scope. This article explains what the levels mean, how to determine the correct one and how the link with the execution classes of EN 1090-2 works.
What ISO 5817 actually covers
ISO 5817 applies to fusion-welded joints in steel, nickel, titanium and their alloys, for material thicknesses from 0.5 millimetres. The standard lists dozens of imperfection types, numbered according to ISO 6520-1, and gives limit values for levels B, C and D for each. Think of cracks, lack of fusion, porosity, slag inclusions, undercut, excess weld metal, spatter grooves and dimensional deviations of the weld. For some imperfections, such as cracks, the rule at every level is: not permitted. For others, such as porosity, the permitted sizes and quantities shift per level. The standard judges the weld, not the method: it is used in visual testing and as the acceptance criterion for other non-destructive testing.
Level D: moderate
Level D permits the largest imperfections and suits welded work with a limited structural function and low consequences of failure. Within EN 1090-2, level D belongs to execution class EXC1: simple, predominantly statically loaded structures. Note that even at level D, cracks and significant lack of fusion are not permitted. D is not a licence for poor workmanship, but a realistic acceptance level for applications with a large safety margin and no fatigue loading.
Level C: intermediate
Level C is the usual level for most structural applications and corresponds to EXC2 within EN 1090-2, the class covering the bulk of building construction. The limit values for undercut, porosity and weld geometry are clearly stricter than at D, yet remain achievable for a controlled production process with qualified welders. For many workshops, level C is therefore the practical reference point: producing consistently at C keeps rework limited and satisfies the most common contract requirements.
Level B: stringent
Level B sets the strictest requirements and applies to heavily or dynamically loaded structures: bridges, crane runways, fatigue-sensitive details and applications with severe consequences of failure. Within EN 1090-2, B belongs to EXC3; EXC4 requires B with additional requirements, referred to as B+, where the execution specification imposes extra limits on features such as spatter grooves and weld geometry. Level B demands demonstrable craftsmanship, tight process control and more testing: the likelihood of repair rises and with it the cost. Specify B only where the loading or the risk justifies it.
Selecting the right level
The quality level follows in this order:
- From the product standard: EN 1090-2 links the level to the execution class, from D at EXC1 to B with additions at EXC4. See our article on the execution classes.
- From the contract or specification: clients may require a stricter level than the product standard for a project or for individual weld details.
- From the design assumptions: fatigue-sensitive details may locally require a higher level than the rest of the structure.
Record the selected level in the welding procedure specification and the inspection and test plan, so that welder, inspector and client work to the same criterion. A level agreed only at final inspection almost always ends in dispute.
Assessment in practice
The first check against ISO 5817 is visual testing to ISO 17637: one hundred percent of the welds, using measuring tools such as weld gauges for throat thickness, excess weld metal and undercut. Supplementary testing, for example magnetic particle or ultrasonic, uses its own acceptance standards linked to the ISO 5817 levels. Important for the assessor: measure and record rather than trusting the naked eye in borderline cases. An undercut of half a millimetre may be acceptable at level C within the stated limits and unacceptable at level B. Independent welding inspection and QA/QC provides an objective judgement, precisely when fabricator and client disagree.
Frequently asked questions
EN 1090-2 links them directly: EXC1 to level D, EXC2 to level C, EXC3 to level B and EXC4 to level B with additional requirements. A contract may impose stricter demands on top, for example level B for specific fatigue-sensitive details within an EXC2 project.
No. Even at level D, cracks and other critical imperfections are not permitted. Level D merely allows wider limit values for imperfections such as porosity, undercut and weld geometry. It remains a measurable acceptance criterion, not an exemption from quality.
No. The level follows from the applicable product standard, such as EN 1090-2 via the execution class, or from the contract and the structural specification. The workshop must know the required level before welding starts and record it in the WPS and inspection plan.
No. Aluminium is covered by the sister standard ISO 10042, which follows a comparable structure with the same levels B, C and D. ISO 5817 covers steel, nickel, titanium and their alloys. The assessment methodology is the same for both standards.
More from the knowledge centre


Have a welding or QA/QC question?
Ask the DEHAAS Welding & Quality Assistant, have your case reviewed by a specialist, or call us directly.